 English
 简体中文
Short answer: At -30C an undercarriage does not fail because the steel turns brittle. Three effects stack up: seals harden and lose elasticity, grease thickens and multiplies start-up torque, and hydraulic oil viscosity rises so motor response lags. Low-temperature NBR seals, cold-rated hydraulic oil and a gearbox oil change cut cold-start torque from 2.4x to 1.5x the ambient figure, validated over 12 consecutive starts in a -30C chamber.
1. Duty profile and failure prediction
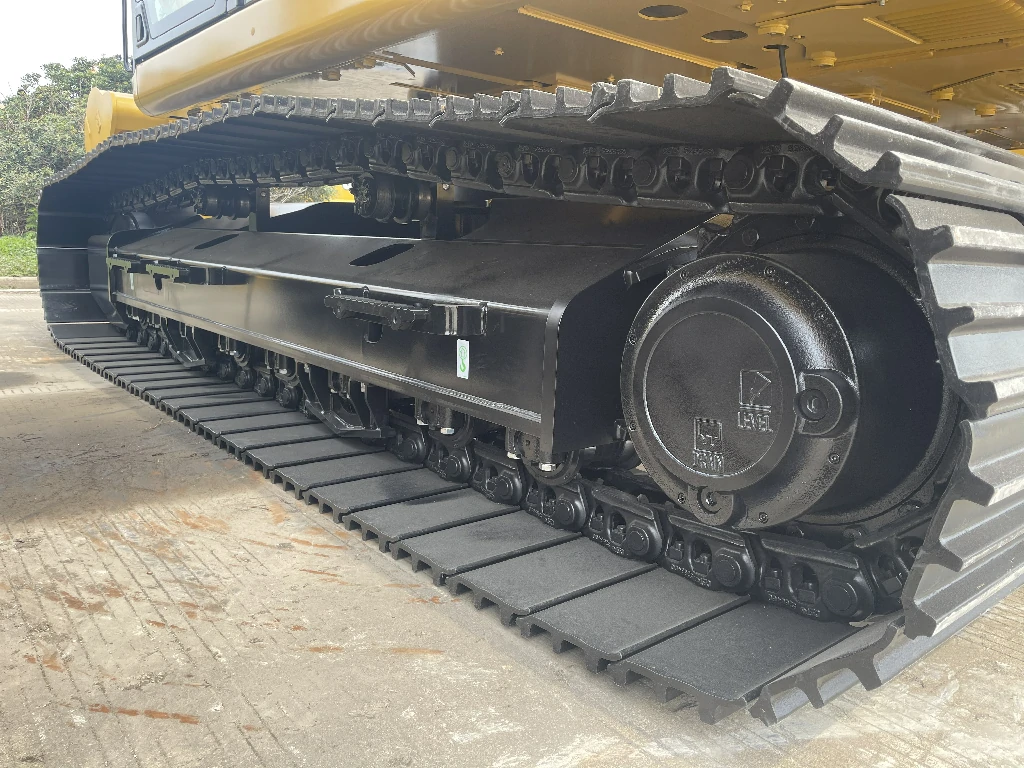
The machine works in a high-latitude mine at -25C to -35C ambient, with two to three cold starts a day and outdoor parking between shifts. The 12-ton steel chassis uses twin motor drive. The standard configuration was well proven above -15C but had no low-temperature data.
The upfront FMEA concentrated on four items: roller lip seals, the tensioner rod seal, final drive gear oil and hydraulic return back pressure. Plate itself was straightforward - specify a grade with validated -40C impact energy and move on.
2. Material and fluid substitution list
Standard NBR seals were replaced with low-temperature NBR rated to -45C brittleness, with polyurethane on critical lips. Grease became a low-temperature synthetic NLGI 1.5. Final drive oil became full synthetic 75W-90 and hydraulic oil the cold-rated anti-wear grade specified by the machine builder.
The tensioner rod was hard-chromed and finished to a finer surface roughness so a stiff cold lip would not be torn. Every rubber item was annotated on the drawing with batch and brittleness temperature, which prevents a later production batch quietly reverting to standard parts.
3. Cold chamber procedure and measured data
The complete chassis soaked at -30C for 12 hours before each start, over 12 cycles. Peak motor current, time to travel 10 m, roller temperature rise and lip leakage were recorded. The standard configuration leaked at the tensioner on cycle three; the revised configuration completed all 12 cycles without leakage.
The cold-start procedure was fixed at the same time: three to five minutes of unloaded low-speed travel to warm the roller cavities, then progressive loading. Full-load gradient climbing from a cold state is prohibited. The rule was written into the delivered cold-weather operating manual.
4. Delivery and first winter follow-up
Four units were delivered and tracked through their first winter. Machines following the procedure reported no seal leakage. The single anomaly came from a site topping up with ordinary gear oil, which pushed start-up torque back up; it cleared after an oil change.
The project turned into a selectable cold-weather package: low-temperature seals, cold grease, cold fluids and the operating manual, triggered by the destination's minimum design temperature rather than added to every export order.
5. -30C Cold Start Comparison
| Metric | Standard build | Cold build | Note |
|---|---|---|---|
| Cold start torque ratio | 2.4x | 1.5x | Relative to ambient start |
| Time to travel 10 m | 42 s | 27 s | After 12 h soak at -30C |
| Tensioner leakage | Cycle 3 | None in 12 cycles | Effect of low-temp seals |
| Roller temp rise (2 h) | 51C | 44C | Lower grease churning drag |
Key takeaways
- At -30C the failure drivers are seal hardening, grease thickening and oil viscosity - not the steel plate.
- Low-temp NBR to -45C, cold NLGI 1.5 grease and full synthetic 75W-90 are an effective combination.
- Warm the roller cavities with 3-5 minutes of unloaded low-speed travel before applying load.
- Offer the cold package as a destination-temperature-triggered option instead of a blanket surcharge.
Further reading
Case Studies · Steel Crawler Undercarriage · FAQ · OEM/ODM
Prepared by the MAGEON engineering team from custom project records and factory load-test data. Figures are engineering references; final selection should follow approved drawings and the actual duty spectrum.